Non-woven Geotextile Factory Production Steps That Ensure Consistent Quality and Durability
2026-09-08
What separates a non-woven geotextile that fails in months from one that outlasts the project itself? At JInseed Geosynthetics Solution, it comes down to a production sequence engineered for consistency at every turn. From raw polymer selection to needle-punching density and final roll inspection, each step is a deliberate lever controlling tensile strength, permeability, and long-term resistance. Here’s the behind-the-scenes process that turns ordinary non-woven fabric into a durable geotechnical backbone—and why skipping a single stage is never an option.
Fibers That Pass the First Cut
Not every fiber that shows up in a sample makes it past the initial screening. The ones that survive that first cut tend to share a few quiet traits: they hold up under tension without snapping unexpectedly, they don't fray at the edges when you run a thumbnail along the strand, and they keep their color or sheen without needing any special treatment. It's not about being the strongest or the most expensive—it's about consistency. A fiber that behaves the same way on a humid afternoon as it does in a dry workshop is the one worth keeping on the bench.
There's also a tactile honesty to fibers that pass. They don't slip through your fingers like they're trying to escape, and they don't leave a powdery residue or a greasy film behind. When you twist a small bundle between thumb and forefinger, you can feel the individual strands aligning rather than fighting each other. That kind of cooperation under pressure is something you learn to recognize after handling enough rejects. The fibers that make it are rarely the flashiest in the lot; they're the ones that make the next step in the process feel less like guesswork.
At the end of that first culling, what's left is a short list of materials that can actually carry a project forward. The rest get swept aside, not because they're worthless, but because they'd demand too many compromises later on. A fiber that passes the first cut is one that lets you work with a clear head, trusting that the foundation won't shift once you start building on it.
Laying the Web Without Weak Spots
Every layer of a web stack can hide a fracture that only shows up under pressure. Teams often focus on the front door—login pages, payment forms, the main API—while leaving side windows open through outdated libraries, unpatched servers, or overly permissive internal endpoints. A practical first pass is mapping every data path from input to storage and assigning a clear owner to each segment, so no component drifts into neglect.
Input handling is where many small cracks turn into full breaks. Anything arriving from a browser, mobile app, or third-party webhook should be treated as hostile until proven otherwise. Use parameterized queries instead of string concatenation, escape output for its final context, and enforce role-based checks on both the client side and the server side. These steps remove a large share of injection and privilege escalation risks without slowing down development.
Weak spots also appear over time, not just at launch. A web system that was solid last quarter can develop gaps through rushed hotfixes, new third-party scripts, or misconfigured cloud storage. Keep monitoring focused on anomalies—unusual login times, unexpected file changes, traffic spikes to internal routes—and make alert review a weekly habit rather than an afterthought. Pair that with periodic dependency audits and short, targeted penetration tests, and the web stays stronger than the sum of its parts.
Needling and Bonding for Tensile Toughness
Mechanical needling drives barbed needles through a fiber web, forcing filaments to reorient and entangle in the thickness direction. This creates a quasi-three-dimensional network that resists crack propagation more effectively than a flat, layered sheet. The repeated penetration also breaks some fibers and redistributes their ends, which adds a degree of strain redistribution under load instead of a single weak plane failing all at once.
Bonding then locks this entangled architecture into place. Thermal or chemical bonding at fiber intersections prevents the loops and knots from slipping when tension is applied, so the load is shared across a larger volume. If the bond points are spaced too densely, the material turns brittle; too sparse, and the entanglements unravel. The right balance boosts tensile toughness by allowing local fiber pull-out and friction to absorb energy before final rupture.
Thermal Setting That Locks Dimensions
When fibers are heated under controlled tension, their molecular chains relax and then re-form in a new alignment that resists further movement. This process, often called heat setting, fixes the yarns and fabric loops in place so they no longer pull back to their original shape after washing or wearing. The key is to hold the material at a specific temperature for just long enough—too little heat leaves the structure unstable, while too much can scorch the surface or make it brittle. In practice, mills run trials on sample batches to find that narrow window where the width and length stay locked without compromising hand feel or dye uptake.
One overlooked aspect of dimensional stability is how the cooling phase affects the final set. After reaching the target temperature, the fabric must be cooled while still under tension, otherwise the relaxed chains have room to creep back toward their pre-set state. Some factories use chilled rollers or forced air to speed this step, but even ambient cooling works if the line speed is slow enough. The result is a fabric that lies flat on the cutting table and doesn't grow or shrink unpredictably when steam hits it during garment pressing. For tightly woven or knitted constructions, this thermal locking effect can reduce shrinkage to less than one percent in both directions.
Different fiber types respond to thermal setting in distinct ways. Synthetics like polyester and nylon require temperatures near their glass transition point, while cellulosic fibers such as cotton need a resin or crosslinking agent to hold dimensions after heat. Blends add complexity because each component has its own ideal set range—setting for one might under- or over-process the other. Skilled operators often rely on trial swatches and precise thermocouple readings rather than generic oven settings, because even a ten-degree shift can mean the difference between a stable fabric and one that twists or curls on the roll. The locked dimensions aren't just a lab metric; they determine how well a garment holds its seams and silhouette through repeated laundering.
In-Line Checks That Catch Flaws Early
Catching a mistake right as it happens saves a lot more than fixing it later. In-line checks are small verification steps built into the actual work flow, not tacked on at the end. They might look like a quick dimension measurement after a cut, a syntax check after a code block, or a consistency review after drafting a section. Because they happen so close to the action, the person doing the work can correct course immediately, while the context is still fresh.
The real value shows up when multiple small checks accumulate. Instead of one big inspection at the finish line, you get a series of low-friction moments that keep defects from compounding. A tiny flaw in an early stage can turn into a costly rework if it travels downstream. In-line checks cut that chain by making quality part of each step, not a separate event.
Teams that adopt this approach tend to ship more predictable results. The checks don't have to be elaborate—often a simple yes/no question or a quick visual scan is enough. The key is placing them where errors are most likely to appear and making them easy to do without breaking rhythm.
Final Proofing Before Rolls Leave the Floor
Every roll gets a last hard look under the right light before it ships. We check seam alignment, edge trimming, and surface finish piece by piece, not just by sampling. It's the kind of slow, deliberate pass that catches the tiny flaws nobody wants to sign off on.
Warping, chatter marks, and residual burrs are the usual suspects here. If a roll doesn't sit flat on the inspection table or the mic shows even a slight deviation from spec, it gets pulled and reworked on the spot. Nothing leaves until it reads clean.
This final proofing step isn't about speed. It's about making sure the roll that arrives at your dock is exactly the roll we said we'd make, with no excuses and no surprises.
FAQ
Polypropylene tends to be lighter and more cost-effective, but it can degrade faster under prolonged UV exposure unless stabilizers are added. Polyester handles higher temperatures and offers better resistance to creep under sustained loads, so it often ends up in reinforcement applications where long-term tensile strength matters more than initial price.
The carding machine aligns fibers predominantly in the machine direction, which creates a bias in strength unless a cross-lapper is used to lay the web at an angle. Adjusting the cross-lapper speed and layering pattern lets the factory balance machine-direction and cross-direction strength, reducing weak spots across the roll.
Needle punching interlocks fibers mechanically with barbed needles, creating a felt-like structure with high elongation and excellent puncture resistance. Thermal bonding, by contrast, melts a portion of fibers to fuse contacts, producing a thinner, stiffer fabric that works well for filtration but may sacrifice some conformability on uneven subgrades.
Many lines use a scanning gauge that measures basis weight and thickness continuously across the web. If readings drift outside set tolerances, the system either flags the section or automatically adjusts the feed rollers. Some factories also stop the line to pull a small sample for manual verification every few thousand square meters.
Higher punch density increases the number of fiber-to-fiber contacts, which raises tensile strength and reduces pore size. However, going too far can damage fibers and create thin spots. The key is finding a density range where the fabric still allows adequate water flow while maintaining enough integrity to survive installation stresses and long-term soil pressure.
Excess moisture turns to steam during extrusion, creating voids or weak points in the filaments. In staple fiber processes, damp fiber can clump and feed unevenly into the card, leading to thin and thick patches. Pre-drying or conditioning the material to a consistent moisture level prevents these defects and keeps the line running with fewer stops.
UV stabilizers are often added directly to the polymer melt or applied as a surface treatment after bonding. Calendering can be used to smooth the surface and lock in dimensions by slightly flattening the fiber intersections. Some products also receive a heat-setting pass to reduce shrinkage when the fabric is later exposed to warm soil or direct sunlight.
Accelerated weathering tests expose samples to intense UV light and moisture cycles in a laboratory chamber, simulating months or years of outdoor exposure in a few weeks. Coupled with tensile tests before and after exposure, these results give a reliable estimate of how much strength the geotextile will retain over its design life.
Conclusion
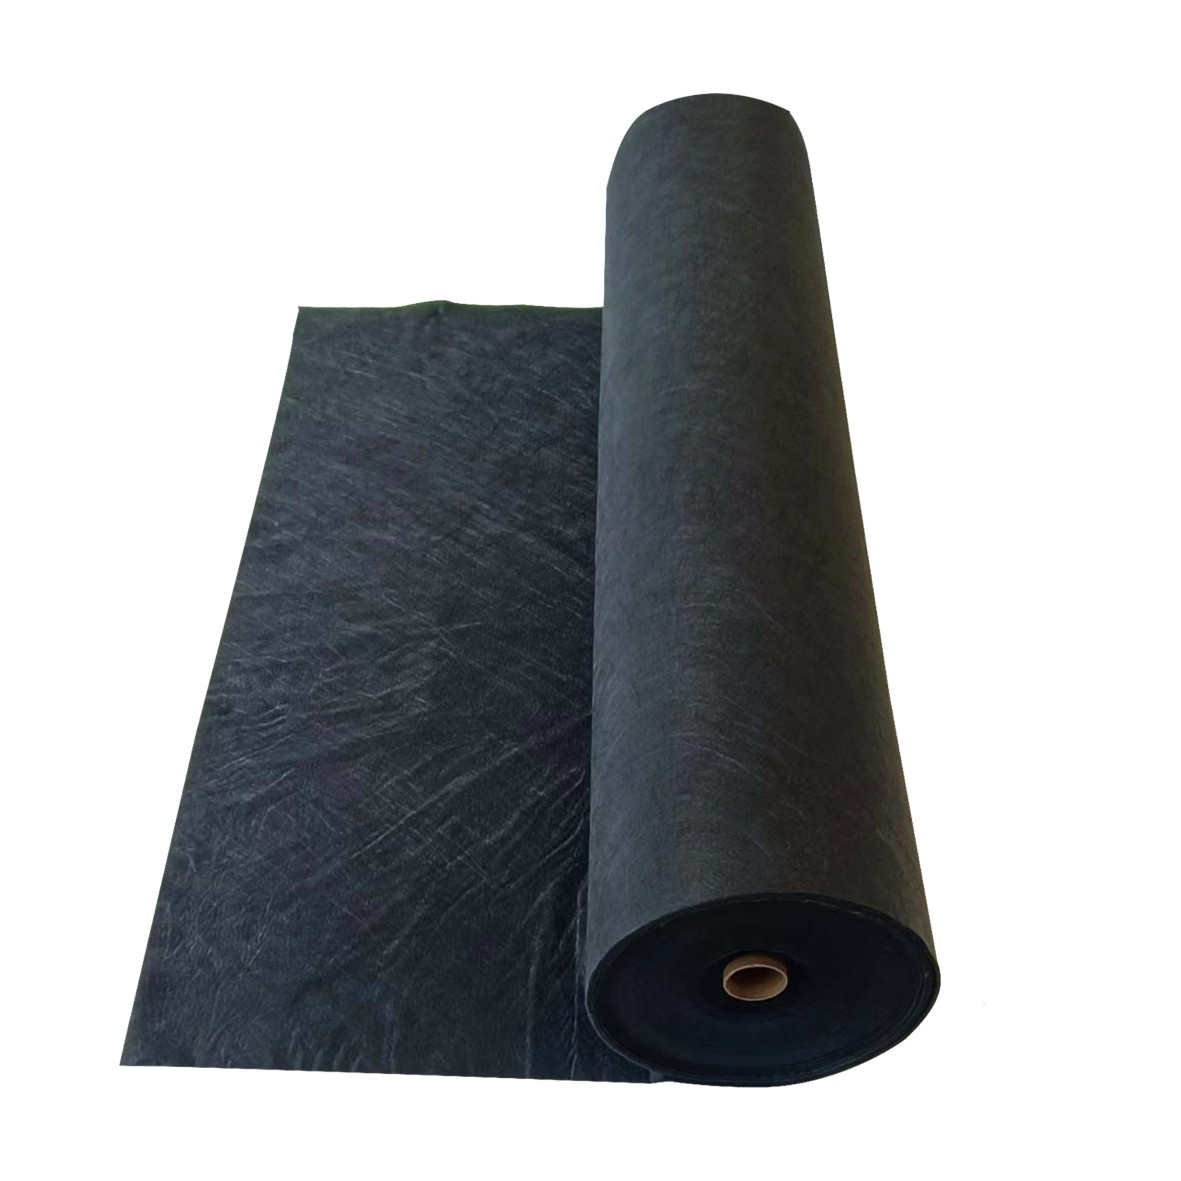
The production line only works as well as the fiber that feeds it. Before anything else, incoming staple fibers are tested for denier, crimp stability, and tensile strength, and batches that fall outside a narrow tolerance band are rejected outright. What survives then goes through carding and cross-lapping, which builds a layered web with deliberately randomized fiber orientation—this prevents weak spots from forming along any single axis. Needle punching follows, using barbed needles arranged in a staggered pattern to entangle the fibers into a dense, cohesive structure. It is this mechanical bonding, more than any chemical additive, that gives the fabric its early tear resistance and puncture strength.
After needling, the material passes through a thermal setting oven where heat is applied just long enough to relax residual stress and lock in the final width and length. Fabrics that would otherwise shrink or creep under load are stabilized here, so the roll dimensions stay true on site. In-line cameras and weight sensors scan the full width at production speed, catching thin spots, needle streaks, and density drift before they become hidden inside the roll. Finally, samples are pulled from both edges and the center of every master roll and run through grab tensile, CBR puncture, and water permeability tests. Only rolls whose edge and center values stay within a very tight band are cleared for wrapping and shipment.
Contact Us
Contact Person: Jerry Qiu
Email: [email protected]
Tel/WhatsApp: +65 84265294
Website: https://www.jinseed-geo.com