Laser Safety Apron Export: A Complete Guide to Global Compliance and Protection
2026-10-12
Exporting laser safety aprons isn't just about meeting a spec sheet—it's about proving your protection holds up under the scrutiny of regulators in the US, EU, and beyond. One overlooked standard can turn a full container into a warehouse liability. That's why forward-thinking suppliers rely on LASERPAIR to navigate every compliance layer, from EN 60825 to FDA laser notice requirements. Ahead, we dissect the export roadmap—covering certifications, labeling, and quality checks—so you can move laser safety aprons across borders with zero guesswork.
Mapping Certification Requirements Across Key Markets
Understanding certification demands in different regions is less about memorizing rulebooks and more about recognizing patterns in how regulators think. A single product often faces a patchwork of technical standards, labeling norms, and documentation expectations that shift the moment you cross a border. Teams that map these requirements early tend to spot overlaps, reuse test data, and avoid the costly back-and-forth of late-stage compliance fixes.
The practical approach starts with a matrix that separates mandatory certifications from voluntary marks, then layers in market-specific timelines and renewal cycles. For instance, what passes as a self-declaration in one country may demand third-party lab testing in another, even when the underlying safety principles are nearly identical. Keeping this map alive—updated with regulatory notices and enforcement trends—turns certification from a one-time hurdle into a repeatable advantage.
Rather than treating each market as an isolated challenge, successful teams build reusable evidence packages: core test reports, risk assessments, and technical files that can be adapted with minimal rework. The goal is not just to enter a market, but to do so with enough margin to absorb unexpected changes without stalling the launch.
Decoding Laser Class Ratings for Apron Selection
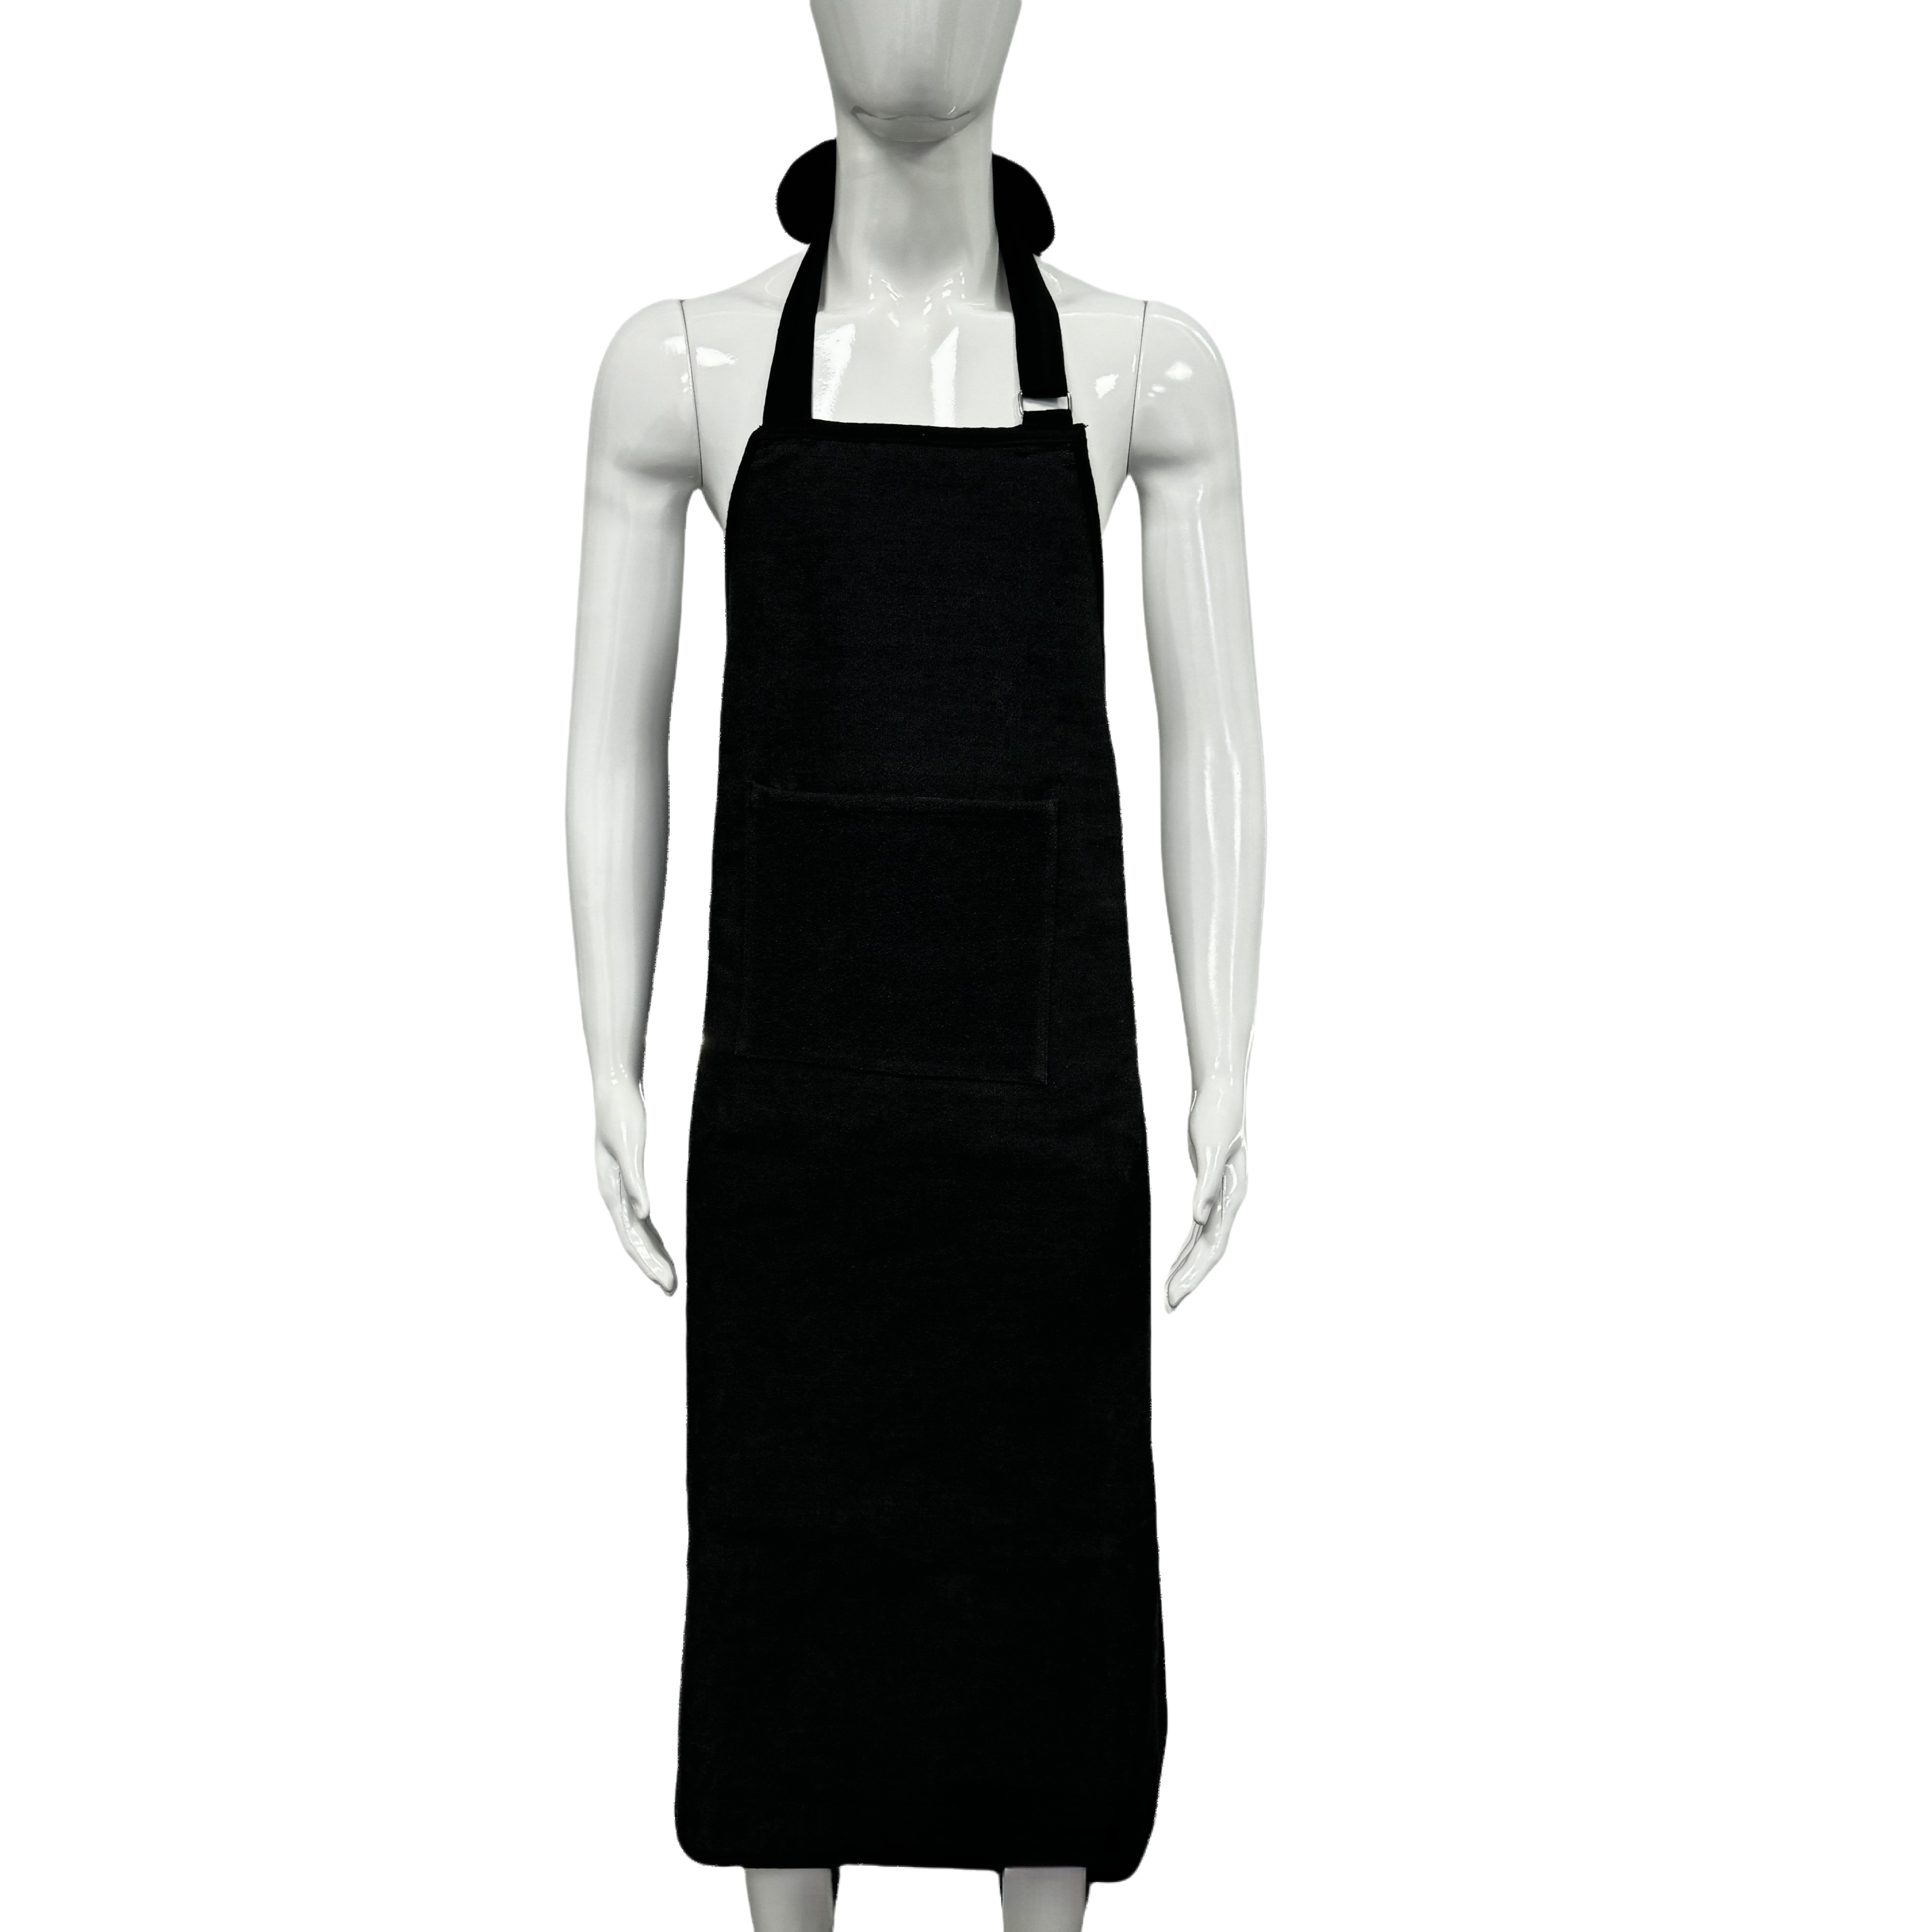
Laser class ratings exist to communicate how much danger a given system poses without requiring everyone to read a physics textbook. Classes 1 and 2 are effectively safe for normal use, which means an apron is usually overkill unless your workflow involves deliberate beam manipulation far outside the intended enclosure. The conversation changes once you reach Class 3B or Class 4, where diffuse reflections and direct skin contact can cause real burns or ignite clothing. For those higher classes, an apron stops being a suggestion and becomes part of the primary barrier between your torso and an invisible, often unforgiving beam.
The tricky part is that a laser's class rating alone won't tell you which apron to buy. You need to match the apron's optical density and damage threshold to the specific wavelength and power density you're working with. A fabric that blocks a 532 nm green beam beautifully might be nearly transparent at 10,600 nm from a CO2 cutter. Look for aprons labeled with test data across the full range of wavelengths your facility uses, and pay attention to whether the rating covers direct hits or only scattered light. Some materials degrade quickly under continuous-wave exposure, so peak power and dwell time matter just as much as the nominal class number.
Practical selection often comes down to the jobs that make you lean into the beam path: alignment, maintenance, or clearing a jam while the laser is in a service mode. In those moments, a front-closure apron with shoulder coverage and a high neckline provides more protection than a basic bib. If the material is stiff or hot, people will leave it hanging on a hook, so balance protection against wearability. Ultimately, decoding class ratings for apron selection means treating the label on the laser as a starting point, then checking wavelength-specific test reports before trusting your skin to any fabric.
The Hidden Costs of Non-Compliant Shipments
When a shipment misses a single regulatory detail, the obvious fine is usually the smallest expense. Customs holds can trap containers for weeks, triggering terminal storage charges, demurrage, and per-diem fees that continue around the clock. Brokers and internal compliance teams then spend hours reconstructing paperwork, often at overtime rates, while the cargo sits untouched.
The pressure to recover lost time creates a second wave of costs. Companies air-freight replacement stock to keep assembly lines moving, pay premium rates for expedited legal or consulting help, and sometimes have to re-export or destroy goods that cannot be cleared for entry. None of this appears in the original freight quote, so finance teams rarely see the true cost until the quarter closes.
There's also a quieter long-term penalty. Repeated non-compliance raises the likelihood of inspections on future shipments, slows down clearance for otherwise clean cargo, and can trigger contractual penalties with customers who expected on-time delivery. Over a year, these hidden costs quietly reduce working capital and make planning less reliable.
Choosing Materials That Pass Muster Abroad
What clears a compliance check in one country can stall at the border in another. A material that breezes through local building codes might still conflict with a stricter chemical restriction, a different flame-spread rating, or an unfamiliar certification scheme overseas. The first step is to stop treating certifications as a generic stamp and instead map each target market's mandatory marks and test methods before you commit to a supplier.
Look beyond the headline logo. CE marking in Europe and UL recognition in North America both sound reassuring, but they rest on very different assumptions about installation, use, and end-of-life handling. For electronic enclosures, the plastic's UL 94 V-0 rating may satisfy a US inspector, while an EU buyer expects a RoHS and REACH declaration that covers substances the US rule never mentions. Ask for the exact test reports, not just the certificate number, and check whether the lab that issued them is accredited under the target region's framework.
The safest approach is to build a short list of materials that already hold multiple region-specific approvals, then confirm those approvals are current and tied to the exact grade you plan to purchase. A formulation change at the factory can quietly invalidate a past pass, so request batch-level traceability and a written change-notification clause in your supply agreement. Where no single material fits every market, weigh the cost of running a few extra tests against the cost of a rejected shipment at a foreign port.
From Factory Floor to Foreign Port: Documentation Essentials
A shipment rarely gets delayed because the goods themselves are wrong; it gets delayed because a commercial invoice lists a vague product description or omits the country of manufacture. Customs officials don't have time to guess, so they hold the container and wait for corrected paperwork.
The packing list matters more than most shippers expect. Carton counts, weights, and dimensions must line up with the bill of lading, or the discrepancy gets flagged at the destination terminal. Once that happens, the consignee often pays storage and inspection fees before anyone even argues about whose mistake it was.
The certificate of origin is easy to overlook until a broker points out that it changes the duty rate. A free trade agreement might lower the tariff from 8 percent to zero, but only if the document is filled out correctly and signed before departure. Getting these details sorted on the factory floor beats negotiating with a foreign port agent after the ship has already sailed.
Staying Ahead of Changing Import Rules for Protective Gear
Import regulations for protective equipment rarely stay still for long. A standard that passed inspection last quarter can suddenly require updated certification documents, revised labeling, or a completely different testing protocol. Buyers who assume last year's paperwork will carry them through the next shipment often end up with cargo held at the border and expensive demurrage fees piling up.
The practical approach is to treat compliance as an ongoing conversation rather than a one-time checklist item. Keep a direct line open with your overseas suppliers and ask them to flag any draft regulatory changes they hear about through local industry groups. At the same time, subscribe to updates from the relevant customs agencies—not the promotional newsletters, but the actual tariff and standards bulletins. A short monthly review of these sources costs little and can prevent a rushed scramble when a new rule takes effect mid-order.
FAQ
For Europe, the CE mark under the Personal Protective Equipment Regulation (EU) 2016/425 is mandatory, with EN 60825-4 serving as the key harmonised standard for laser guards and protective aprons. In North America, there is no single federal product approval, but ANSI Z136.1 and OSHA 29 CFR 1910.132 set the practical benchmarks. Buyers in Canada may also expect alignment with CSA Z94.3 or provincial occupational health rules. Exporters should verify the exact standard version required by each destination because test reports older than five years are sometimes rejected.
Optical density must be tested against the actual wavelength, pulse duration, and power density of the laser in use. A credible test report from an ISO 17025 accredited laboratory should list the exact wavelength range, maximum irradiance or exposure time, and the achieved OD value. Simply stating a high OD on the label is not enough; the certifier or importer will want to see that the apron material was challenged under conditions matching the laser class, including possible degradation from repeated pulses.
Missing the notified body identification number when the apron is classified as Category III PPE is a frequent issue. Other recurring problems include omitting the wavelength range and optical density from the permanent label, using non-durable ink that fades after cleaning, and failing to include the manufacturer's name and address in a legible format. Some exporters also leave off the batch or serial number, which makes recalls or post-market surveillance nearly impossible.
If the apron is designed to be worn by a person, it falls under PPE regulations and must follow that conformity assessment route. If it is intended to be fixed to a laser machine as a barrier or curtain, it may be treated as a machine guard under Directive 2006/42/EC in the EU, or as an engineering control under OSHA in the US. The classification changes the technical file requirements, the type of CE marking, and the customs harmonised system code, so exporters should confirm the intended use with the buyer before preparing documents.
Beyond the commercial invoice and packing list, many ports ask for a signed Declaration of Conformity, the relevant test reports, and sometimes a certificate of origin. Countries with strict import controls may also require an import permit or a safety data sheet for the apron materials. Keeping the technical file in a structured format - with drawings, risk assessments, and user manual - helps clear inspections faster because officers can quickly verify traceability.
A material that blocks a 1064 nm Nd:YAG beam may be nearly transparent at 10.6 µm from a CO2 laser. For CO2 systems, the apron often needs a flame-resistant outer layer combined with a dense, thermally stable core. For visible and near-infrared lasers, specialised absorbing dyes or carbon-loaded polymers are used. The key is matching the material's absorption curve to the exact emission spectrum of the laser, not relying on a generic laser-proof label.
The user manual should include a pre-use visual check for cracks, burns, discoloration, or delamination. It must explain how to clean the apron without damaging the protective layer - usually mild soap and water, never solvents or bleach - and how to store it flat or hung, away from direct sunlight. Buyers also need a clear end-of-life policy, such as retirement after a certain number of wash cycles or after any incident where the apron was directly hit by the beam.
The core protective material often can be shared, but the final product usually needs minor changes. The EU requires the CE mark, a notified body number for Category III PPE, and instructions in the official languages of the destination countries. The US expects labeling aligned with ANSI Z136.1 and OSHA hazard communication, while Canada may demand bilingual English-French markings. It is more cost-effective to plan for regional labeling variants from the start than to retrofit them after a shipment is held at customs.
Conclusion
Exporting laser safety aprons is rarely a matter of shipping a one-size-fits-all product. A single apron that satisfies EN 207 in Germany may fall short of the FDA’s laser notice requirements in the United States or Japan’s JIS standards. Certification landscapes differ not only by country but also by intended use—medical, industrial, or research. This means manufacturers must map requirements early, focusing on the laser class ratings (such as 3B or 4) that dictate the optical density and wavelength coverage an apron must provide. Overlooking these details leads to costly rejections at customs, but the real damage often goes deeper: delayed orders, rework charges, and a reputation for unreliable compliance. Non-compliant shipments can also trigger audits or import bans that persist long after the initial mistake.
Material selection then becomes a balancing act between protective performance and international acceptance. Fabrics that block specific wavelengths might meet one market’s test methods but fail another’s impact-resistance or flammability clauses. Suppliers should demand third-party test reports aligned with IEC 60825 or ANSI Z136 and keep those records ready for the destination port. Export documentation—certificates of conformity, safety data sheets, and country-of-origin proofs—must match the product exactly; even a minor discrepancy invites scrutiny. Finally, import rules for personal protective equipment are shifting frequently, with some nations tightening labeling and traceability requirements. Staying ahead means monitoring regulatory updates through local agents, participating in standards committees, and treating compliance as a continuous process rather than a one-time checklist. Only then can a manufacturer protect both the end user and its own export pipeline.
Contact Us
Contact Person: Jenny
Email: [email protected]
Tel/WhatsApp: +86 13537713281
Website: https://www.laserpair-safety.com/