Expanded PTFE Gasket Factory Production Techniques for Reliable Industrial Sealing Solutions
2026-11-16
Walk through a chemical plant or refinery and the last component anyone wants to think about is a gasket—until it leaks. At that point, the conversation shifts back to how the expanded PTFE gasket was made, not just what it was made from. Production choices such as expansion rate, density control, and curing conditions largely decide whether a seal holds under aggressive media and thermal cycling. This post unpacks the factory techniques behind reliable industrial sealing and why TAIFNO treats them as non-negotiable.
Where Raw PTFE Resin Meets Factory-Grade Processing
Raw PTFE resin arrives as a fine, waxy powder that clings to everything and resists nearly every solvent known. Turning that powder into usable stock shapes or custom parts demands more than a standard extrusion line. It calls for controlled compression, precise preforming, and sintering cycles that respect the material's high melt viscosity and tendency to cold-flow under pressure. When these variables are handled correctly, the resulting billets and sheets show uniform density and consistent mechanical properties from edge to edge.
Practical processing also means accepting that PTFE cannot be injection molded or recycled like most thermoplastics. Instead, it must be ram extruded, compression molded, or skived from sintered cylinders. Each method favors different geometries and tolerances, and small shifts in dwell time or cooling rate can change the final crystallinity and wear characteristics. Shops that understand these trade-offs can produce parts that survive in seals, valve seats, and chemically aggressive environments without the blistering or stress cracking seen in poorly processed stock.
The real advantage appears when raw resin is paired with production tooling built for PTFE's quirks. Heated mandrels, slow cooling zones, and dust containment measures all contribute to repeatable output. Rather than treating PTFE as a drop-in replacement for nylon or acetal, factory-grade processing treats it as its own discipline—one where batch records, pressure curves, and sintering profiles decide whether a finished part lasts months or years in the field.
From Solid Billet to Flexible Gasket in Controlled Expansion Stages
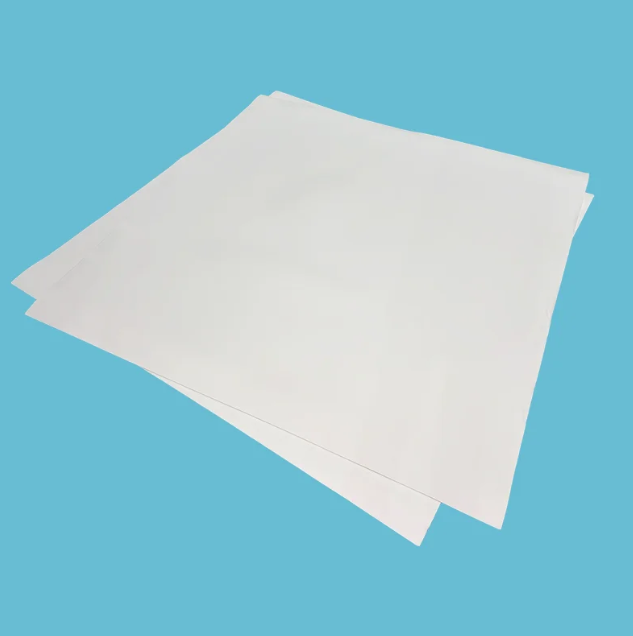
Starting with a compact graphite billet, the material is pushed through a sequence of controlled expansion steps rather than a single thermal shock. Each pass is run at a slightly different temperature and dwell time, which lets the layers separate into long, worm-like strands without tearing. That staged approach keeps the bulk density steady and prevents the kind of uneven loft that shows up later as weak spots near the flange face.
The expanded material is then calendered into a continuous sheet under stepped pressure. Early passes set the thickness, while later passes build the interlocking grain that gives the gasket its recovery after compression. The sheet is cut to size only after its flexibility and density have stabilized, so the finished gasket conforms to minor flange irregularities and still holds a reliable seal under thermal cycling.
Sintering Heat Curves That Give Expanded PTFE Its Seal Strength
Most discussions of expanded PTFE stop at temperature, time, and pressure. Yet the real control over seal strength lives in the shape of the sintering heat curve itself. Ramp rates, hold plateaus, and cooling profiles determine whether the polymer chains knit into a dense, load-bearing network or remain loosely fused and prone to cold flow under flange load. A curve that climbs too quickly traps residual stresses at the node-fibril boundaries. A curve that lingers too long at peak temperature overshoots the melt state, collapsing the very porosity that gives the material its conformability. The result is a gasket that either cracks during installation or creeps into the gap over service life.
The strongest seals come from curves that treat sintering as a three-stage sequence: a slow approach through the crystalline transition, a carefully bounded peak plateau, and a controlled return through recrystallization. During the approach, the material expands and then relaxes as the crystalline domains lose their long-range order. If the heating rate is uneven across the sheet thickness, the surface fuses while the core remains unconsolidated, creating a weak interface hidden inside the finished part. A well-designed curve adds a brief intermediate hold just below the melting point to equalize temperature throughout the cross-section before any significant flow begins.
Cooling is often treated as an afterthought, but it is where much of the final strength is decided. Rapid quenching freezes in a finer crystalline structure and can boost tensile strength, yet it also builds in residual stress that shows up later as warpage or dimensional change. Slow, staged cooling produces a more relaxed structure with better creep resistance and lower stress relaxation under sustained bolt load. The practical art is balancing these two demands: enough crystallinity to resist extrusion, enough amorphous mobility to seal against rough flange faces. Small changes in the cooling slope—sometimes only a few degrees per minute—shift the material from a stiff, unforgiving sheet into a resilient seal that holds torque over thousands of thermal cycles.
Holding Tight Thickness and Density Tolerances for Reliable Sealing
Thickness variation in sealing materials rarely announces itself until a flange has been torqued, heated, and cycled. A difference of only a few thousandths of an inch can shift the compressive load across the face, leaving one edge over-compressed while another area never reaches the minimum seating stress. Tight thickness tolerances give assembly teams a predictable starting point, so the same bolt pattern and torque sequence produce the same gasket contact pressure on every joint.
Density can drift even when thickness looks stable, and that drift changes how the material responds under load. A low-density pocket may collapse too quickly, reducing recovery when thermal expansion pushes the flanges apart; a dense band may feel rigid and resist conforming to minor surface irregularities. Holding density within a narrow range keeps porosity, compression set, and permeation behavior consistent enough for the seal to survive pressure spikes and temperature swings.
Practical control often depends on measuring both properties in process rather than relying on final inspection alone. Laser thickness gauges, beta transmission sensors, and automated sampling at the calender or extrusion line allow adjustments before a full batch drifts out of specification. When those measurements are tied to the actual sealing application, the tolerances become more than a quality check—they describe the window where the material can still do its job.
The Test Bench Routine Behind Every Batch of Industrial Gaskets
Every batch leaves the curing press with a small stack of witness coupons cut from the same sheet. Those coupons go straight to the bench, not to a shelf. The first check is thickness recovery after a controlled crush cycle; the gauge reads before, at load, and again thirty minutes after release. If the rebound curve drifts outside the narrow band on the chart, the whole lot is held before it ever reaches a packing table.
Leakage testing here is done with nitrogen, not air, because the smaller molecule exposes flaws that a looser setup would miss. Each gasket sits against a grooved steel plate at the minimum bolt load specified for the material class. Technicians watch for the pressure needle to settle and stay flat for a full two minutes. A pass is not just “no bubble.” It means the drop stays under five millibars, and the trace on the recorder shows no slow bleed.
The bench also logs hardness across three points and checks for surface cracks under a low-angle light. Those numbers go into the batch record next to the compound lot, press operator, and cure time. If a gasket comes back from a customer, the same routine is run again on the returned piece and on retained samples. That comparison usually tells more than any specification sheet.
Adapting Production Techniques to Aggressive Media and High Pressures
Working with aggressive media changes the rules of manufacturing in ways that go beyond simply choosing a tougher material for the equipment. The first practical step is often to map out exactly where erosion, corrosion, or chemical attack is most likely to begin. This means looking past the obvious contact points and paying attention to welds, seals, and small radius transitions that can concentrate stress or trap reactive fluids. Once those weak spots are identified, it becomes easier to decide whether the better route is a harder surface treatment, a shift in toolpath to reduce dwell time, or a complete redesign of the component geometry to avoid dead zones where media can stagnate.
High pressures add a second layer of constraint, especially when they are combined with fluctuating temperatures or abrasive particles. Under sustained mechanical load, even small material defects can grow quickly, so process control has to be tighter than in conventional machining. Tooling choices, feed rates, and cooling strategies all have to be rebalanced. In many cases, the most reliable approach is to slow down certain operations intentionally, not because the machine cannot go faster, but because a more deliberate pace helps preserve surface integrity and reduces the chance of micro-fractures that later become failure points.
There is also a strong case for treating these production challenges as a system problem rather than a series of isolated fixes. A coating that performs well in lab tests may fail on the shop floor if the base material expands at a different rate or if the cleaning step leaves a residue that weakens adhesion. Similarly, high-pressure sealing depends on the interaction between finish quality, fastener tension, and the actual shape of the mating surfaces under load. Teams that get the best results tend to iterate across these variables together, using short production runs and inspection data to refine the process instead of relying on a single material upgrade or a generic best practice.
FAQ
Resin grade, particle size distribution, and contamination levels are verified first. The PTFE resin is then blended and sieved to remove agglomerates, because any inconsistency in the raw feed shows up later as uneven sheet density or weak spots in the gasket.
Stretching the PTFE creates a network of fine fibrils and micropores. That structure makes the sheet softer and more compressible, so it can fill small flange irregularities at low bolt loads while still resisting creep under temperature cycling.
Sintering locks the stretched fibril structure in place. If the temperature curve is too fast or uneven, the sheet can shrink, develop hard spots, or lose its dimensional stability, which leads to gaskets that do not sit flat on the flange.
Large sheets are cut by CNC knife cutting, waterjet cutting, or die cutting depending on the size and quantity. For thicker or dimensionally critical gaskets, cutting speed and tool sharpness are adjusted to avoid compressing the edges or leaving a fuzzy cut surface.
Density, tensile strength, thickness tolerance, and leak rate are tested on each production batch. Visual inspection also looks for cracks, inclusions, or uneven surface texture because these defects can create a direct leak path under pressure.
The material carries the chemical resistance of PTFE, so it withstands acids, caustics, solvents, and high-purity media without leaching or degrading. The soft expanded structure also reduces the need for aggressive fillers, making it safer for lined or fragile flanges.
The flange surface should be cleaned and checked for flatness before installation. Bolts are tightened in a controlled star pattern with a calibrated torque wrench, and the gasket should be centered so it does not protrude into the flow path or get pinched unevenly.
Yes. Thickness, sheet density, and outer dimensions can be adjusted to suit large-diameter heat exchangers, narrow flanges, or low-load plastic piping. Some workshops also supply adhesive-backed or color-coded sheets for easier installation and traceability.
Conclusion
Production starts well before the first gasket takes shape. Raw PTFE resin is checked for particle size distribution and flow behavior, then pressed into a solid billet under carefully controlled compression. That billet is not simply sliced into sheets; it moves through staged expansion where temperature and pull speed are adjusted in small increments. Rushing this step leads to uneven fibril formation, so operators watch the material stretch rather than relying on a fixed recipe. The sintering phase matters just as much as expansion. Heat curves are tuned to let the expanded structure lock in without overshooting into brittle territory. A poorly managed curve can erase gains made earlier, leaving surface cracks or weak spots that only appear under flange load.
Once the sheet is formed, thickness and density are measured at multiple points across each production run. Calipers and density checks are not treated as final gatekeeping steps; they inform real-time adjustments to calendering and tension. Every batch also goes through a bench routine that includes leak simulation, recovery after compression, and exposure to representative chemicals. For applications involving aggressive media or high pressures, the process parameters shift instead of relying on the same product with false confidence. Filler choices, expansion ratios, and sintering dwell times are altered to handle acids, solvents, or elevated temperatures. The result is a gasket that holds a seal where standard PTFE would creep or blow out.
Contact Us
Contact Person: Tommy Xiao
Email: [email protected]
Tel/WhatsApp: 8615651509888
Website: https://www.ptfe-factory.com