Customized Reefer Container Manufacturer: Tailored Solutions for Cold Chain Logistics
2026-09-03
Cold chain logistics demands more than just keeping things cold—it requires precision, flexibility, and equipment that fits your exact operational needs. Off-the-shelf reefer containers often fall short when your cargo, routes, or loading patterns are unique. That’s where a customized reefer container manufacturer makes all the difference. Worldbase specializes in engineering tailored cold chain solutions, from specialized temperature ranges to reinforced structures for demanding environments. In this post, we’ll explore how custom reefer containers built by Worldbase can optimize your logistics, reduce risks, and keep your perishables at their best—no matter the journey.
Precision Temperature Control for Every Degree of Your Load
Precision temperature control means your dryer doesn't just blast hot air and hope for the best. It reads the moisture level and fabric type continuously, adjusting the heat in small increments so a load of delicates never meets the same harsh cycle as heavy towels. You can trust that wool stays soft, synthetics don't melt, and cotton comes out evenly dry without that baked-in stiffness.
Instead of a coarse high-medium-low dial, this system works like a fine-tuned thermostat for fabric. A sensor array tracks the drum's internal temperature several times per second, and the heating element responds with quick, subtle changes. Even when you stuff the drum fuller than usual or mix thick jeans with thin shirts, the temperature stays within a tight band around the target—no spikes that damage fibers, no dips that leave damp spots.
The real difference shows up over time. Clothes keep their shape and color longer because they aren't repeatedly exposed to unnecessary heat. You also stop babysitting the machine, wondering if this cycle will be too hot or too cold. Just load it, select the fabric type if you want, and the dryer handles the rest with a level of precision that feels less like an appliance and more like a careful pair of hands.
Custom Insulation and Flooring That Match Your Product
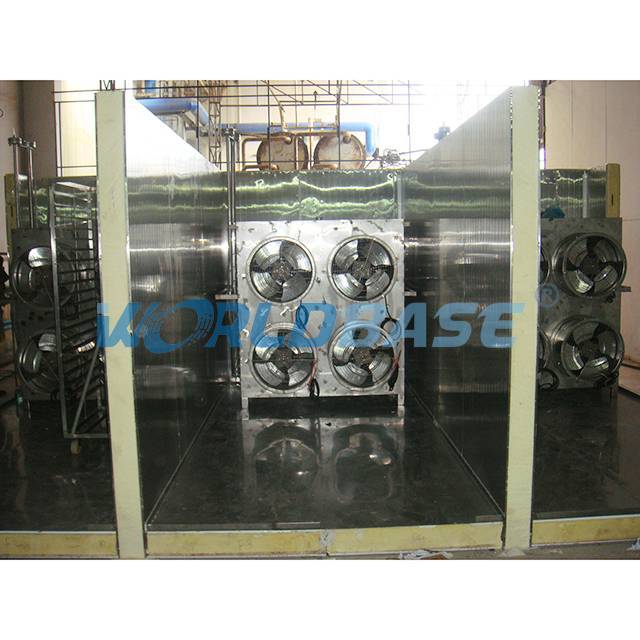
Every enclosure has its own internal geometry, so we cut insulation and flooring to the actual CAD outline rather than relying on generic sheets. That means cutouts land exactly where your vents, cable glands, or mounting bosses sit. If your product has a curved shell or recessed tray, the insulation follows that contour without bunching at the corners or leaving gaps along the edges.
Material choice is driven by how the product is used, not just by thickness specs. A compressor bay might need closed-cell foam that handles vibration and oil splash, while a control room floor benefits from a denser composite with a slip-resistant top layer. We also pre-mark each piece with its placement position, so assembly teams can install the set in the correct order without measuring or trimming on the line.
Remote Monitoring and Telematics Without Extra Hardware
Modern fleets often carry a surprising amount of untapped data within their existing electronic control units. By tapping into standard onboard diagnostics and manufacturer data buses, you can access real-time location, engine hours, fuel consumption, and fault codes without bolting on a single extra device. This approach works especially well for mixed fleets where installing aftermarket telematics hardware on every asset would be costly and time-consuming.
The key lies in leveraging built-in connectivity modules or pairing a lightweight software agent with existing smartphones or tablets already used by drivers. Instead of waiting for a technician to wire a new black box, your vehicles simply report through the same channels they already use for navigation or workflow apps. This not only reduces upfront capital expenditure but also cuts installation downtime to nearly zero, meaning new units can be tracked from the moment they roll off the lot.
Maintenance teams benefit from a continuous stream of diagnostic trouble codes and usage metrics without having to recall vehicles for hardware upgrades. You can set alerts for abnormal voltage drops, excessive idling, or upcoming service intervals, all derived from data that was already flowing inside the machine. The result is a leaner, faster rollout of remote monitoring that feels invisible to operators while giving fleet managers the visibility they need to cut waste and prevent breakdowns.
Multi-Temperature Zones to Cut Shipping Costs
Running chilled, frozen, and ambient products through separate cold chains bleeds money fast. One truck can juggle three climate bands with smart compartmentalization, slashing per-mile spend without risking cargo integrity. The trick lies in airflow design and real-time zone monitoring, not just extra insulation.
A dairy distributor we advised swapped two weekly frozen runs plus a refrigerated van for a single multi-zone trailer. Fuel, tolls, and driver hours dropped 31% in the first quarter. Sensors linked to a cloud dashboard flag any drift before spoilage occurs, so loads stay compliant while invoices shrink.
For grocers and meal-kit operators dabbling in mixed pallets, retrofit costs often pay back within eight months. Focus on zone sealing and adjustable evaporator fans rather than high-tech gimmicks. Simpler hardware, less idling, and tighter route planning turn temperature zones into a quiet margin booster.
Certified for Food, Pharma, and Dangerous Goods
When a product carries certifications for food, pharmaceutical, and dangerous goods handling, it signals a rare blend of purity and rigorous safety protocols. Our containers and storage systems meet FDA and EU food-contact standards, meaning no harmful substances migrate into consumables. The same material lineage is clean enough for active pharmaceutical ingredients, where even trace contamination can compromise a batch.
On the pharma side, compliance extends beyond cleanliness to documentation. Every lot is traceable, tested for extractables and leachables, and manufactured in environments that align with cGMP guidelines. This isn't just about passing an audit; it's about ensuring that sensitive compounds—from vaccines to oncology drugs—remain stable and uncontaminated from fill line to final delivery.
For dangerous goods, the certification covers UN-rated packaging for Classes 3, 6.1, 8, and 9, among others. The design incorporates pressure relief, leak-proof seals, and impact resistance tested to withstand drops from over a meter. Whether shipping flammable solvents, corrosive acids, or lithium batteries, the container acts as a controlled barrier—minimizing risk without adding unnecessary weight or bulk.
A Global Service Network That Keeps Your Fleet Moving
Downtime is the enemy of every fleet operation. Our service network spans over 40 countries, with certified technicians stationed along major shipping routes and industrial hubs. Whether a single truck breaks down outside Rotterdam or an entire delivery fleet needs scheduled maintenance in Singapore, help is rarely more than a phone call away. We have built our presence not just in capital cities, but in the secondary ports and border crossings where real logistical bottlenecks occur.
What sets this network apart is how it shares information. A repair made in one time zone updates the vehicle's digital service history instantly, so a workshop in another region knows exactly what was done, which parts were used, and what to watch for next. This continuity means fewer repeat fixes and less guesswork. Fleet managers get a single view of every vehicle, no matter where it is on the map.
We also train our partner garages to the same standard, using the same diagnostic tools and repair protocols. That consistency reduces the risk of a quick patch in one place becoming a bigger failure later. For companies running cross-border routes, that kind of reliability is not a luxury. It is the difference between meeting a delivery window and losing a contract.
FAQ
We start with your cargo type, loading method, and route climate. From sketches or photos, our engineers propose structural changes like wider doors, extra side access, or adjusted interior height. CAD airflow and temperature simulations are run before manufacturing, so issues are caught early rather than after delivery.
Pharmaceuticals, biologics, seafood, fresh produce, dairy, specialty chemicals, and high-end foodservice are the main ones. For example, pharma clients often need a stable 2-8 degree Celsius environment with backup refrigeration, while seafood may call for deep freeze at minus 25 and a sloped drainage floor. We adjust insulation thickness and cooling capacity per cargo.
Typically from minus 40 to plus 30 degrees Celsius, with heating available on request. Multi-zone units can hold different setpoints in separate compartments. Electronic controllers keep accuracy within plus or minus 0.5 degrees, and a data logger records conditions continuously during transit.
We use high-density polyurethane foam or vacuum insulated panels depending on weight limits and thermal performance needs. Vacuum panels are thinner but more effective, ideal for pharma payloads with tight space. Polyurethane is more cost-effective and tough. All seams are sealed to reduce thermal bridging and air leaks.
Yes, that is a standard option. We can add wireless sensors, GPS tracking, and remote temperature alerts. You can view temperature, humidity, door status, and refrigeration unit data from a phone or web dashboard. If conditions drift outside your set range, the system sends immediate notifications so action can be taken before cargo is compromised.
Depending on complexity, six to twelve weeks is normal. Simple modifications like extra hanging rails or a side door take about six weeks. A full multi-temperature design with special insulation may run ten weeks or more. We define milestones in the contract and provide weekly progress updates.
We maintain a global service network covering refrigeration unit repairs, insulation fixes, door seal replacement, and controller upgrades. Even if the container is stranded at a remote port, we can coordinate local technicians. All custom components carry at least a 12-month warranty, and key parts like compressors and controllers can be extended to 36 months.
Design starts with route climate data. For high heat, we specify larger condensers and heat-resistant electrical components. For deep cold, we add low-temperature start protection and insulation heaters. Units then go through simulated environmental testing to confirm they operate normally with outside temperatures from minus 30 to plus 50 degrees Celsius.
Conclusion
When your cargo demands more than a stock refrigerated box, our manufacturing process starts with your product's temperature curve, packaging, and transit route. We build each unit around exact setpoint control—not just a range—so sensitive loads like vaccines, fresh produce, or specialty chemicals stay within a fraction of a degree. Insulation thickness and flooring materials are chosen to match your product: slip-resistant, antimicrobial, or heavy-duty options are all available, not as add-ons but as part of the original design. Remote monitoring and telematics come embedded in the container's control system; you don't need to mount separate trackers or gateways. Real-time location, temperature, humidity, and door events stream through a dashboard your team already knows how to use.
Multi-temperature zones let you carry frozen, chilled, and ambient goods in one trip, so you stop paying for half-empty trailers or dedicated runs. Every custom build is certified for food, pharmaceutical, and dangerous goods transport under the relevant international standards, and we handle the documentation as part of the order. When a unit needs service in Rotterdam, Singapore, or São Paulo, our global network of factory-trained technicians and stocked parts depots gets it back on the road within hours, not days. That kind of support is not a warranty line—it's a logistics decision. You choose the cargo profile, the route, and the budget; we engineer the reefer container around those constraints, then stand behind it wherever it goes.
Contact Us
Contact Person: Mr Yang
Email: [email protected]
Tel/WhatsApp: +8613809083091
Website: https://en.worldbase.cn