China Skinning Machine: A Practical Guide for Meat Processors
2026-09-18
Choosing a skinning machine from China isn’t just about picking the cheapest model—it’s about finding equipment that won’t let you down mid-shift. This guide cuts through the noise, offering practical insights for meat processors who need machines that perform day in and day out. You'll also discover why Worldbase has become a go-to for processors tired of compromise. Ready to see what separates a workhorse from a gamble? Let’s get into it.
How Blade Clearance Affects Yield on Different Cuts
Blade clearance is rarely the first thing operators check when yield drops, but it often explains why identical machines produce wildly different scrap rates. When the gap between the cutting edges is too wide for the material, the blade stops shearing and starts tearing. Fibers stretch, coatings crack, and small fragments break away instead of separating cleanly. Those fragments end up as waste, and the remaining edge may need a second trim pass, which directly reduces the number of usable pieces per sheet or batch.
The effect is not uniform across cut types. Straight guillotine cuts tolerate very little clearance; even a slight overshoot causes the material to fold over the lower blade and leave a ragged lip. Shear cuts are more forgiving because the angled entry reduces peak force, but too much gap creates a pronounced burr that must be deburred. Crush cuts, often used for thin films or paper, rely on a controlled pinch between the blade and anvil. If that pinch is inconsistent, the cut line wanders and the web splits unpredictably, turning what should be a continuous roll into short, unusable strips.
A practical starting point is to set blade clearance between 4% and 8% of material thickness for shear cuts, then tighten or loosen based on the edge condition. For guillotine cuts on rigid stock, keep the gap near zero but not so tight that the blades gall. Run short test strips after every adjustment, and record the clearance that gives the cleanest break without excessive blade wear. Small changes of a few thousandths of an inch can shift yield by several percentage points, especially on laminated or coated materials where a single torn layer forces the entire part into the reject bin.
Comparing Stainless Steel Grades in Chinese Skinning Machines
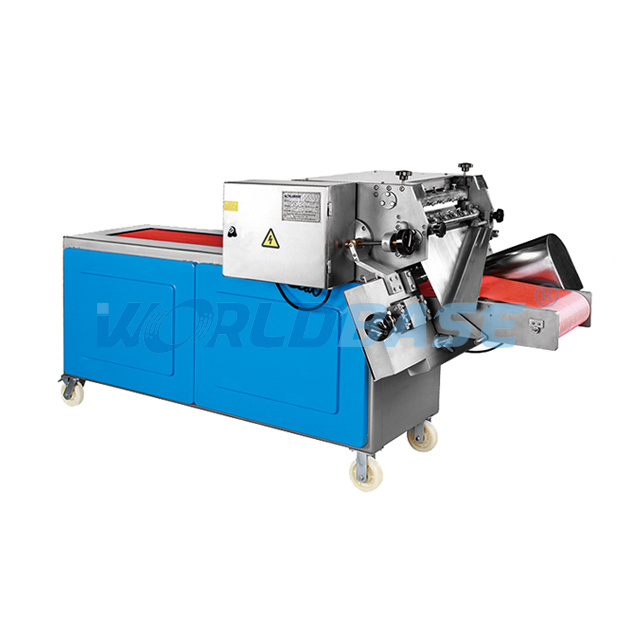
Stainless steel grades in Chinese skinning machines are not interchangeable once you look past the surface finish. Most factories default to 304 because it balances corrosion resistance, weldability, and cost for standard meat or vegetable processing. Grade 316 shows up in machines designed for seafood, brined products, or frequent exposure to salt and acidic cleaning agents — the added molybdenum makes a real difference in pitting resistance. At the lower end, 201 is still used in some budget models, but its lower nickel and chromium content means it can develop tea staining or rust spots far sooner, especially around welded joints and under gaskets.
From a maintenance standpoint, 304 is forgiving; it tolerates typical food-contact cleaners and occasional exposure to moisture without immediate damage. However, if a skinning machine runs multiple shifts with saline washdowns or citric acid-based sanitizers, 316 pays for itself by avoiding surface degradation that eventually contaminates product or requires early frame repair. Chinese manufacturers often build the same model with either 304 or 316, so the upgrade cost is usually modest — though some buyers overlook that 316 also needs proper passivation to perform as expected.
Choosing between grades should come down to the actual process, not just the initial quote. For most land-based meat or fruit peeling lines, 304 holds up fine and keeps replacement parts affordable. Saltwater fish skinning, high-chloride environments, or aggressive CIP chemicals tip the balance toward 316. If a supplier quotes 201 for a wet or salty application, treat that as a red flag; the short-term savings rarely survive the first year of daily cleaning. Request mill test reports and check the thickness at the drum and blade housing, because some low-cost machines use thinner 304 sheet that warps or dents before the grade itself fails.
The Case for Adjustable Speed Drives in Small Plants
Small plants often operate on tight margins, where every kilowatt-hour and maintenance hour counts. Fixed-speed motors running pumps, fans, or conveyors at full output regardless of demand waste energy and accelerate component wear. An adjustable speed drive changes that equation by matching motor speed to the actual process requirement. In a small facility, the savings from reduced electricity use and fewer mechanical shocks can directly improve the bottom line without requiring a large capital outlay or a dedicated engineering team.
Beyond energy savings, adjustable speed drives bring a level of process control that fixed-speed setups simply cannot offer. Soft starting eliminates the sudden inrush current that strains both the electrical supply and the driven equipment. Operators gain the ability to fine-tune flow rates or line speeds from a simple keypad, responding to shifting production needs within seconds. For a small plant with limited staff, this means fewer manual adjustments, less downtime from belt slippage or valve wear, and more consistent output quality without constant supervision.
The payback period in small plants is often shorter than commonly assumed, especially when utility rebates and reduced peak demand charges are factored in. Many newer drives are compact enough to fit into existing enclosures, and setup has become far simpler with auto-tuning features and plain-language menus. Rather than viewing this technology as a luxury reserved for large operations, small plant managers should see adjustable speed drives as a practical tool to stretch resources, lower operating costs, and build resilience against fluctuating production demands.
What Processing Managers Often Overlook About Safety Guards
Many processing managers treat machine safety guards as static, set-and-forget components. They often overlook that guards must match the specific operation and material flow, not just generic enclosures. For example, a guard that fully encloses a conveyor may create a new hazard during jam clearing, forcing workers to remove panels repeatedly and bypass interlocks. That's a recurring oversight.
Another overlooked area is the interaction between guards and routine maintenance. Managers assume presence of a guard means protection, but if the guard obstructs lubrication points or inspection windows, technicians will either remove it permanently or work around it in unsafe ways. The real issue is design for maintainability, not simply adding more metal.
Also, safety guards are rarely checked for wear or alignment after installation. Vibration, impacts, and thermal cycling can gradually make a guard less effective or interfere with moving parts. Processing managers who focus on throughput metrics often miss these slow degradations until an incident or an audit forces a fix.
Simple Routines That Prevent Roller and Bushing Wear
Most wear on rollers and bushings doesn't start with a dramatic failure—it begins quietly, in the gaps between greasing schedules and the few extra degrees of misalignment nobody bothered to correct. A simple habit of checking bearing temperatures by hand every shift can catch a dry or over-tightened roller long before metal starts to gall. Train operators to treat a warm roller as a warning, not a nuisance, and to investigate immediately rather than waiting for the next scheduled maintenance window.
Cleanliness is another underrated routine. A quick wipe of exposed roller paths and bushing seals with a lint-free cloth removes abrasive dust that acts like sandpaper on every rotation. Pair this with a simple visual gauge for chain or belt tension—not a high-tech sensor, just a marked bracket or a consistent finger-pressure test—so that tension stays within the manufacturer's band. When tension drifts, rollers and bushings take the punishment, wearing into oval shapes that then accelerate their own destruction.
Finally, rotate your inspection focus. Instead of always checking the same high-visibility components, choose one roller or bushing at random each week and spend five minutes looking for hairline cracks, seal leakage, or buildup at the edges. This breaks the routine blindness that lets small problems grow unnoticed. Combined, these low-cost habits often outperform expensive condition-monitoring systems because they build a culture of attention, not just a log of measurements.
Questions to Ask Chinese Suppliers Before Shipping
Before you release final payment or confirm shipment, get the supplier to walk you through every step of the loading and dispatch process. Ask for precise carton dimensions, gross weight, and pallet count—not just a rough estimate. Also confirm the Incoterm: if it's FOB, you need the forwarder's details and booking confirmation, not just the supplier's word. Many delays happen because the supplier books space with a local agent that doesn't match your forwarder, so pin down the actual vessel name and ETD.
Demand photos or a short video of the goods being packed, labeled, and loaded into the container, with the shipping marks clearly visible. Ask if they will provide a pre-shipment inspection report (if you arranged one) and a final packing list with actual quantities. Clarify who handles export customs and what documents they'll send—commercial invoice, packing list, bill of lading draft. If your payment terms include a balance before shipment, agree on a deadline for those documents after the vessel sails. And don't forget to ask about any last-minute substitutions or color/material changes: sometimes suppliers swap components to meet deadlines, and you want that in writing before the container leaves.
FAQ
Focus on frame rigidity, blade adjustment range, and whether the manufacturer uses food-grade stainless steel on all contact surfaces. Ask for a demo video running frozen or chilled pork skin, not just soft fat.
The gap has narrowed significantly in the past five years. Many Chinese units now share similar gearbox designs and blade hardness, but you may need to pay closer attention to electrical component brands and spare part availability. For high-volume lines, European machines still lead in servo precision; for mid-volume butcher shops, Chinese machines often deliver better value.
Plan on 800 to 1,200 kg per hour for pork skin removal with a 550 mm working width, assuming consistent operator feeding. Fish or poultry skin may run slower due to texture. Do not rely on peak numbers in brochures; ask for a timed test with your own product.
Pneumatic or spring-loaded pressure shoes usually outperform fixed manual settings when the incoming fat layer varies. If your product is uniform, a simple handwheel adjustment is fine. Check that the blade can be changed in under ten minutes without special tools.
Most exported models include CE-style guards, emergency stop bars, and low-voltage controls. However, training should still cover lockout procedures before blade changes and never bypassing the safety interlocks. Request a manual in English and a video walkthrough before shipping.
Lubricate the main drive chain or gearbox every 40 operating hours, inspect blade sharpness daily, and check alignment after every 200 hours. Replace plastic wear strips before they show deep grooves. Keep spare blades and a drive belt on hand to avoid downtime.
Standard wear parts like blades and pressure shoes usually ship within 3 to 5 business days by express. For larger components such as motors or gearboxes, plan for 10 to 20 days depending on your location. Always confirm the manufacturer stocks parts rather than making them to order.
Yes, but you will need to adjust blade depth, pressure, and possibly switch to a coarser feed roller. Beef skin is thicker and tougher, so a machine with a stronger motor (at least 1.5 kW) and hardened blade is recommended. Test both products if possible before buying.
Conclusion
Getting the most out of a China skinning machine starts with dialing in blade clearance for each specific cut—pork belly, beef flank, or chicken thigh all behave differently, and a gap that works for one can tear another, costing yield. Meanwhile, not all stainless steel is equal: 304 resists corrosion in wet packing rooms but 316 holds up better against salt and acid from brines, and some Chinese suppliers quietly swap grades unless you pin them down. For small plants, adjustable speed drives aren't a luxury; running slower on delicate skins and faster on tough hides reduces waste and lets one machine handle multiple species without a rebuild.
Safety guards get overlooked because they seem obvious, yet many processors remove them for faster cleaning and never put them back correctly—leaving pinch points exposed where rollers meet the frame. Simple daily routines, like wiping down rollers and greasing bushings before the first shift, prevent the kind of wear that leads to uneven skinning and expensive downtime. Before you commit to a shipment, ask Chinese suppliers for actual test videos on your product, detailed steel certifications, and the exact tolerance range for blade adjustment—if they hesitate, keep looking.
Contact Us
Contact Person: Mr Yang
Email: [email protected]
Tel/WhatsApp: +8613809083091
Website: https://en.worldbase.cn