Best Ultrasonic Coating System for Precision Thin-Film Applications
2026-09-21
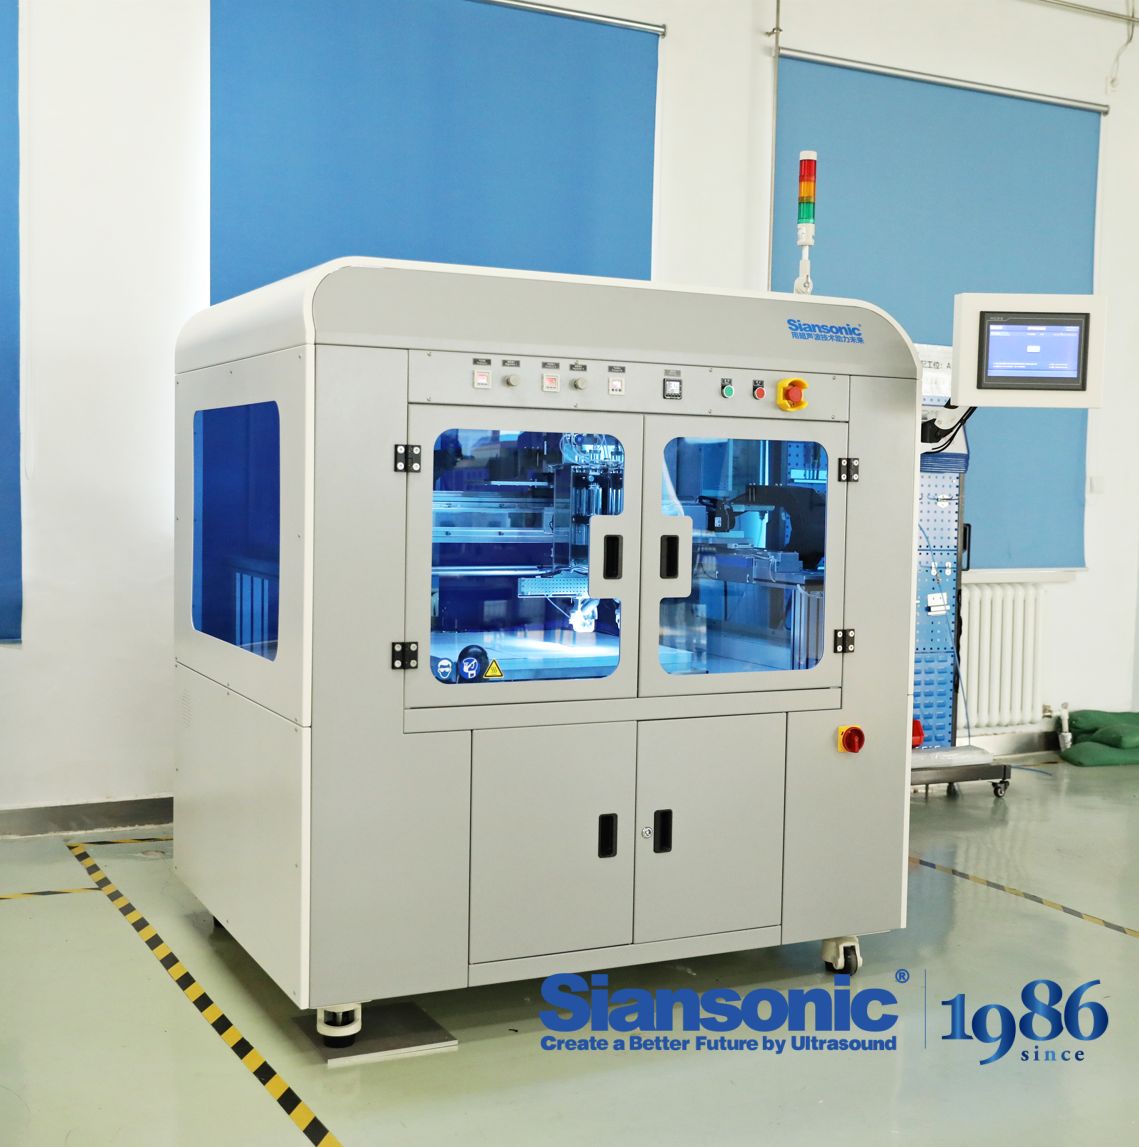
Uniform thin films don’t happen by accident. They demand a coating process that eliminates mist, waste, and edge defects—something traditional nozzles struggle with. Ultrasonic systems solve this, but not all are equal. This is where Siansonic stands out. Before you choose a system for your precision thin-film application, here are the factors that actually matter.
What Really Happens When You Switch to Ultrasonic Thin-Film Coating
Switching to ultrasonic thin-film coating changes the entire texture of your application process. Traditional methods rely on pressure or high heat to bond layers, but ultrasonic energy breaks up the coating fluid into microscopic droplets that self-level on contact. The result is a surface that feels less like a painted-on layer and more like the material itself has been subtly altered — smoother at the edges, with none of the orange-peel effect you'd expect from a spray pass.
The real shift shows up in how the coating behaves under stress. Because the ultrasonic nozzle never touches the substrate, you avoid the micro-scratches and uneven thickness that come with blade or roller systems. Thin films become more predictable: a 2-micron layer stays within ±3% tolerance across a curved surface, where a conventional dip coating might drift by 10% or more. Engineers who make the switch often mention the strange absence of bubbles — the vibration literally shakes trapped air out of the liquid before it lands.
What catches most people off guard is the reduction in waste. Ultrasonic atomization uses nearly all the coating material, so overspray drops from typical 30–40% down to under 5%. You stop buying extra coating just to account for drift, and cleanup time shrinks because there's no caked-on residue around nozzles or edges. The first few runs feel almost too clean, as if the machine isn't working — until you measure the film and realize it's exactly where you wanted it.
Why Uniform Layers Start at the Nozzle, Not the Recipe
The usual assumption is that a finely tuned slicer profile—layer height, extrusion multiplier, print speed—will deliver even layers. But the plastic doesn’t care about those numbers until it exits a physical opening. At the nozzle, molten filament is squeezed through a tiny orifice where surface finish, land length, and temperature distribution decide how smoothly the bead lays down. A recipe can call for 0.2 mm layers, but if the nozzle’s inner bore is rough or the tip has even slight wear, the actual extrusion width oscillates from one line to the next.
Pressure inside the melt zone matters more than most settings. A short, polished land length creates less resistance, so extrusion starts and stops cleanly. Longer or poorly machined lands cause lag, oozing, and width variation that no amount of flow compensation can fix. Brass nozzles move heat quickly and keep the melt stable, while hardened steel often needs a bump in temperature just to maintain the same fluidity—this is a hardware adjustment, not a recipe fix.
The easiest way to test this is to swap nozzle sizes or brands without touching the profile. Same layer height, same speed, same material—yet the surface finish and layer registration change immediately. That’s because uniform layers begin at the point of extrusion. Clogs, internal burrs, or uneven heating at the nozzle tip override the cleverest slicing parameters. Before chasing more advanced settings, inspect the nozzle, clean the melt path, and confirm the orifice is round and free of deformation.
Where Precision Coating Systems Outperform Spin Coating
Spin coating might be the default choice in many labs, but it throws away most of the coating fluid. A typical spin process can lose 90% or more of the dispensed material to centrifugal force, which becomes a serious problem when working with expensive perovskite precursors, quantum dot inks, or custom biological reagents. Precision coating systems—particularly slot-die and ultrasonic spray heads—apply fluid only where it’s needed, often achieving material utilization above 95%. That difference alone can determine whether a formulation is economically viable beyond a few test coupons.
Once substrates move beyond small, round wafers, spin coating’s uniformity falls apart. Large glass panels, flexible films, and rectangular solar cells all show edge beads, radial striations, or center-to-edge thickness drift under spin coating. Precision systems maintain a constant coating gap and controlled fluid delivery across the full width, so a 300 mm panel or a roll of polymer web can be coated with the same thickness profile at the start and the end. Slot-die coating, for example, handles widths from a few centimeters to over a meter without changing the fundamental process physics.
There’s also the question of repeatability when moving from manual lab work to production. Spin coating depends heavily on ramp rates, exhaust conditions, and even ambient temperature around the spinner, which are hard to lock down outside a cleanroom. Precision coating systems let you set pump flow rate, stage speed, and coating gap directly, and many include in-line thickness monitoring for closed-loop adjustment. That means a process developed on a bench-top unit can be transferred to a pilot line with far less re-optimization than a spin recipe.
Materials That Play Nicely with Ultrasonic Deposition
Ultrasonic deposition really shines with low-viscosity inks and dispersions—think under about 30 centipoise. Materials like PEDOT:PSS, silver nanowire suspensions, and dilute metal-oxide nanoparticle inks (ZnO, ITO, TiO2) tend to atomize cleanly without clogging the nozzle. Keeping the average particle size below a tenth of the nozzle orifice diameter also makes a noticeable difference, since larger agglomerates can disrupt the standing wave at the tip and lead to spitting rather than a fine mist.
Solvent choice matters just as much as the solute. Water, ethanol, isopropanol, and modest amounts of higher-boiling co-solvents like propylene glycol monomethyl ether work well because they balance evaporation rate and droplet formation. If the solvent flashes off too quickly, you get crusting around the nozzle; too slowly, and the wet film may sag before drying. Some fluoropolymers such as PVDF in acetone or MEK have also proven surprisingly friendly, provided the solution is kept dilute enough for the ultrasonic energy to break it into uniform droplets.
Not everything belongs in an ultrasonic coater. Heavy pastes, highly filled slurries, and resins above roughly 100 centipoise usually need to be thinned before they can be atomized effectively, and even then the extra dilution can change the final film properties. However, a short pre-treatment with a probe sonicator or the addition of a compatible surfactant sometimes brings marginal materials into range—especially when the goal is a thin, conformal layer rather than a thick build-up.
Stopping Defects Before They Ruin a Thin-Film Run
Real-time surface inspection has become the quiet backbone of high-yield coating lines. Rather than waiting for a post-run review to reveal pinholes, streaks, or delamination, operators now catch the earliest signs of trouble while the web is still moving. A subtle shift in reflectance or a faint ripple in thickness often shows up long before the defect becomes visible to the naked eye, which means the adjustment happens at the speed of the process, not after the damage is done.
Process data tells the same story from another angle. When vacuum pressure, line speed, and deposition rate are tracked together, small drifts stop looking like noise and start looking like warnings. Integrating those signals with visual inspection creates a feedback loop that lets a line correct course before a single bad roll reaches quality control. In practice, that is the difference between a short pause to recalibrate and a costly strip-and-recoat of an entire batch.
Setting Up a Benchtop System for Repeatable Results
Getting repeatable readings on a bench rarely comes down to the instrument’s spec sheet—it’s the unglamorous stuff around it. Start by locking down your cabling: use the same test leads every time, mark which ports they plug into, and don’t coil excess wire in a tight loop unless you want an accidental inductor. Power matters too. A cheap wall adapter that dips under load will make your reference voltages wander, so either use a linear supply or at least log the rail with a multimeter before trusting any downstream numbers.
Build a startup ritual and stick to it. Let the gear warm up for twenty minutes, run a quick sanity check against a known resistor or voltage reference, and write the result in a notebook—not just in software. When a measurement does drift, the log will tell you if it’s the room temperature, a tired connector, or something you changed last Tuesday. I’ve saved more setups by cleaning a slightly oxidized BNC jack than by recalibrating the entire chain.
FAQ
The most reliable way is to run a gage R&R on your own substrates with the material you plan to use. Pay attention to the spray cone stability over a full shift, not just a five-minute demo. Systems that log flow rate and nozzle power continuously tend to expose drift early.
They underestimate how much the solvent blend matters. Ultrasonic atomization is gentle, but if the solvent evaporates too quickly, you get dry aerosol that doesn't level properly. Adjusting the co-solvent ratio and keeping the nozzle tip cool usually fixes most edge defects.
Pinholes from oversized droplets and edge buildup from uneven traverse speed are the big ones. A good system with programmable acceleration zones at the start and end of each pass will reduce edge beads dramatically without manual touch-ups.
For precision films on thin or flexible substrates, yes. Vacuum hold-down stops the material from lifting or shifting during coating, and a heated stage shortens the drying window so droplets don't have time to migrate. Without these, you often chase thickness variations that aren't really caused by the sprayer.
Many systems can, but it depends on particle size and dispersion stability. You'll want a nozzle with a larger orifice and continuous recirculation of the suspension. Fixtures that let you flush the tip between runs also help, since settling in the nozzle is the main cause of streaking.
Ask for the raw droplet size distribution and the actual spray width at your working distance—not just a snapshot under ideal conditions. Also compare how the pattern changes at the start and end of a pass. That transient behavior is where a lot of systems fall short in real production.
It's equally important. A nozzle with excellent atomization will still produce uneven films if the stage vibrates or the path speed isn't smoothly controlled. Look for linear motors or at least high-quality ball screws with low backlash, and verify the path repeatability in the tens of microns or better.
Use a spray pattern that matches your part geometry instead of rastering a large rectangle. Program the shut-off and trigger points precisely so the spray only activates over the substrate, not the surrounding fixture. Small changes like this often cut sample prep material use by half.
Conclusion
Swapping a spin coater for an ultrasonic coating system changes the entire dynamic of thin-film work, and the first thing you notice is how much less material you actually need. Because the nozzle uses high-frequency vibration to break the liquid into a fine mist, the coating lands exactly where you aim it rather than flying off the edge of a spinning wafer. Uniform layers really do start at the nozzle—if the spray pattern is stable and the flow rate is steady, you get consistent thickness without having to tweak a dozen recipe parameters. This is where precision systems outperform spin coating, especially on small or oddly shaped substrates where centrifugal force simply cannot distribute fluid evenly. Many low-viscosity polymers, nanoparticle inks, and even some biological solutions deposit cleanly with ultrasonic energy, as long as the solvent system doesn't dry too fast in the mist.
Defects tend to creep in from three places: contaminated substrates, unstable atomization, and poor nozzle positioning. Stopping them before they ruin a run means checking the nozzle tip for buildup, keeping the liquid reservoir free of bubbles, and running a quick test pattern before committing a full batch. For a benchtop system, repeatable results come from locking down the same nozzle height, the same scanning speed, and the same substrate temperature every single time. It sounds obvious, but small drifts in these settings cause more failed coatings than any material incompatibility. A good ultrasonic setup lets you save those parameters, swap in a new syringe of coating fluid, and get nearly identical results on the next run. Once you dial in the mist density and overlap, the system does the rest with far less babysitting than older wet-coating methods.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/